H01N2-E
Rubber arc-welding cable, high flexibility, 100/100 V
H01N2-E is the supple welding cable: the same copper and the same welding rubber as H01N2-D, but with a thinner wall. That makes it thinner and easier to coil. For the welder who moves and coils the cable all day.
H01N2-E is a single-core, extra-flexible rubber welding cable to HD 22.6 S2 (VDE 0282-6) / EN 50525-2-81, rated 100/100 V, for the electrode and return leads of electric arc-welding equipment and for the flexible connection of welding transformers, rectifiers and inverters. It is the high-flexibility sibling of H01N2-D: the conductor and the special welding rubber are identical, but H01N2-E has a thinner rubber wall, so for the same copper cross-section it is smaller in diameter, lighter and easier to handle and coil. Choose it where the cable is moved and coiled a lot. The very fine-wire bare copper conductor gives high flexibility; a single special cross-linked rubber layer (over a separator on the conductor) forms the combined insulation and sheath, heat-, spatter-, oil-, ozone- and weather-resistant and flexible in the cold. It suits dry, damp and wet locations and hand-guided, non-forced flexing; it is not intended for fixed installation or continuous forced reeling.
Also known as: welding cable · flexible welding cable
Applications
- Electrode and return leads of hand-guided arc-welding equipment.
- Mobile welding on site and in the workshop, where the cable is moved and coiled all the time.
- Long welding leads: at the same cross-section a thinner, lighter cable that takes up less room on the reel.
What to look out for
- Thinner wall than H01N2-D: more supple, but less resistant to abrasion and being driven over. If the cable is often dragged over a rough floor or driven over, H01N2-D is the sturdier choice.
- Not for fixed installation and not for continuous forced reeling (motorised reel, welding robot); use a reeling or robot cable there.
- Size the cable for the welding current and duty cycle; the thinner sheath does not raise the current rating.
- Conductor
- Very fine-wire stranded bare (plain) annealed copper, class 6 (to 95 mm²) or class 5 (from 120 mm²) to IEC/EN 60228.
- Separator
- Polyester (PET) film or paper tape over the conductor.
- Sheath
- Single special cross-linked rubber layer serving as combined insulation and sheath (polychloroprene / neoprene-based elastomer, compound EM5 to EN 50363-2-2); a thinner wall than H01N2-D for higher flexibility; round; black.
- Core
- Single core; black (other colours on request).
- Rated voltage Uo/U
- 100/100 V (150 V DC).
- Test voltage
- 1.0 kV.
- Standard
- HD 22.6 S2 (VDE 0282-6) / EN 50525-2-81; conductor IEC/EN 60228.
- Flame-retardant
- IEC/EN 60332-1-2.
- Max. conductor temperature
- +85 °C.
- Permitted outer cable temperature, flexing
- −20 °C to +85 °C (fixed down to −35 °C).
- Min. bending radius, flexing
- 6 × outer diameter (at least as flexible as H01N2-D).
Sizes and weights
| Cross-section | R DC 20 °C (Ω/km) | Outer Ø approx. (mm) | Weight approx. (kg/km) |
|---|---|---|---|
| 10 mm² | 1.91 | 7 | 119 |
| 16 mm² | 1.21 | 8.2 | 181 |
| 25 mm² | 0.78 | 9.7 | 270 |
| 35 mm² | 0.554 | 11.1 | 363 |
| 50 mm² | 0.386 | 13.4 | 528 |
| 70 mm² | 0.272 | 15.3 | 716 |
| 95 mm² | 0.206 | 17.6 | 1012 |
| 120 mm² | 0.161 | 19.4 | 1248 |
| 150 mm² | 0.129 | 21.1 | 1520 |
| 185 mm² | 0.106 | 22.9 | 1840 |
H01N2-E or H01N2-D?
H01N2-E
- thinner wall
H01N2-D
- thicker wall
H01N2-E has the same copper and welding rubber as H01N2-D, but a thinner wall. At the same cross-section H01N2-E is therefore smaller in diameter and more supple in the hand. That matters in mobile welding, where the cable is moved and coiled all the time. If the cable mostly has to withstand abrasion and being driven over, choose H01N2-D.
View H01N2-D →H01N2-E or H07RN-F as a supply cable?
H01N2-E
- electrode and return leads
- 100/100 V
H07RN-F
- between mains and welding set
- 450/750 V
H01N2-E is a welding cable for 100/100 V, only for the electrode and return leads. Between the mains and the welding set there is 230 or 400 V, and that calls for a mains cable such as H07RN-F for 450/750 V. So never use H01N2-E as a supply or extension cable, however supple it is.
View H07RN-F →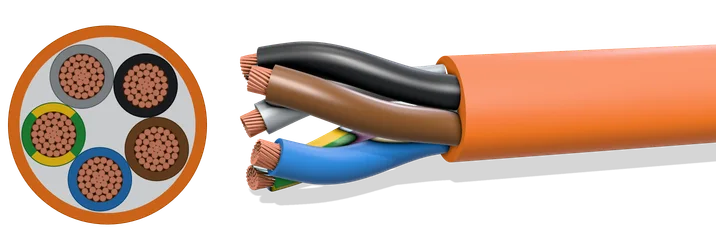
H07BQ-F
Flexible EPR/PUR rubber cable, class 5 Cu, 90 °C
Lead time: On request; the lead time is stated in the quote.
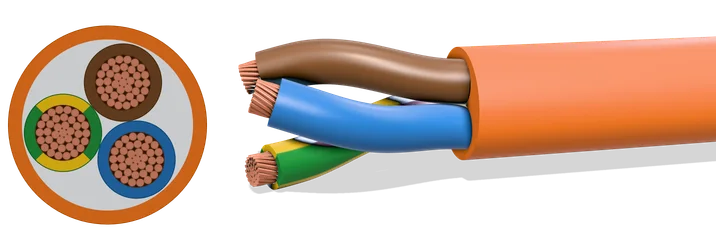
H05BQ-F
PUR-sheathed rubber flexible cable, 300/500 V
Lead time: On request; the lead time is stated in the quote.
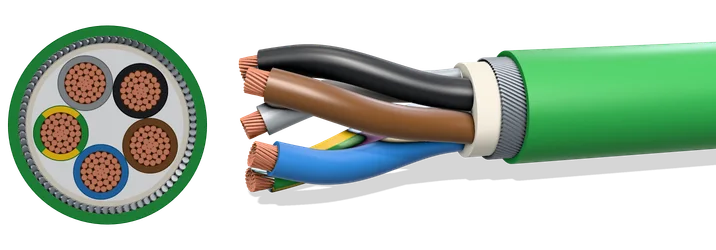
RZ1MZ1-K(AS)
Halogen-free armoured power cable 0.6/1 kV, XLPE/LSZH/SWA/LSZH
Lead time: On request; the lead time is stated in the quote.
Not seeing what you need? Just ask. Our range goes well beyond this list. Ask us →